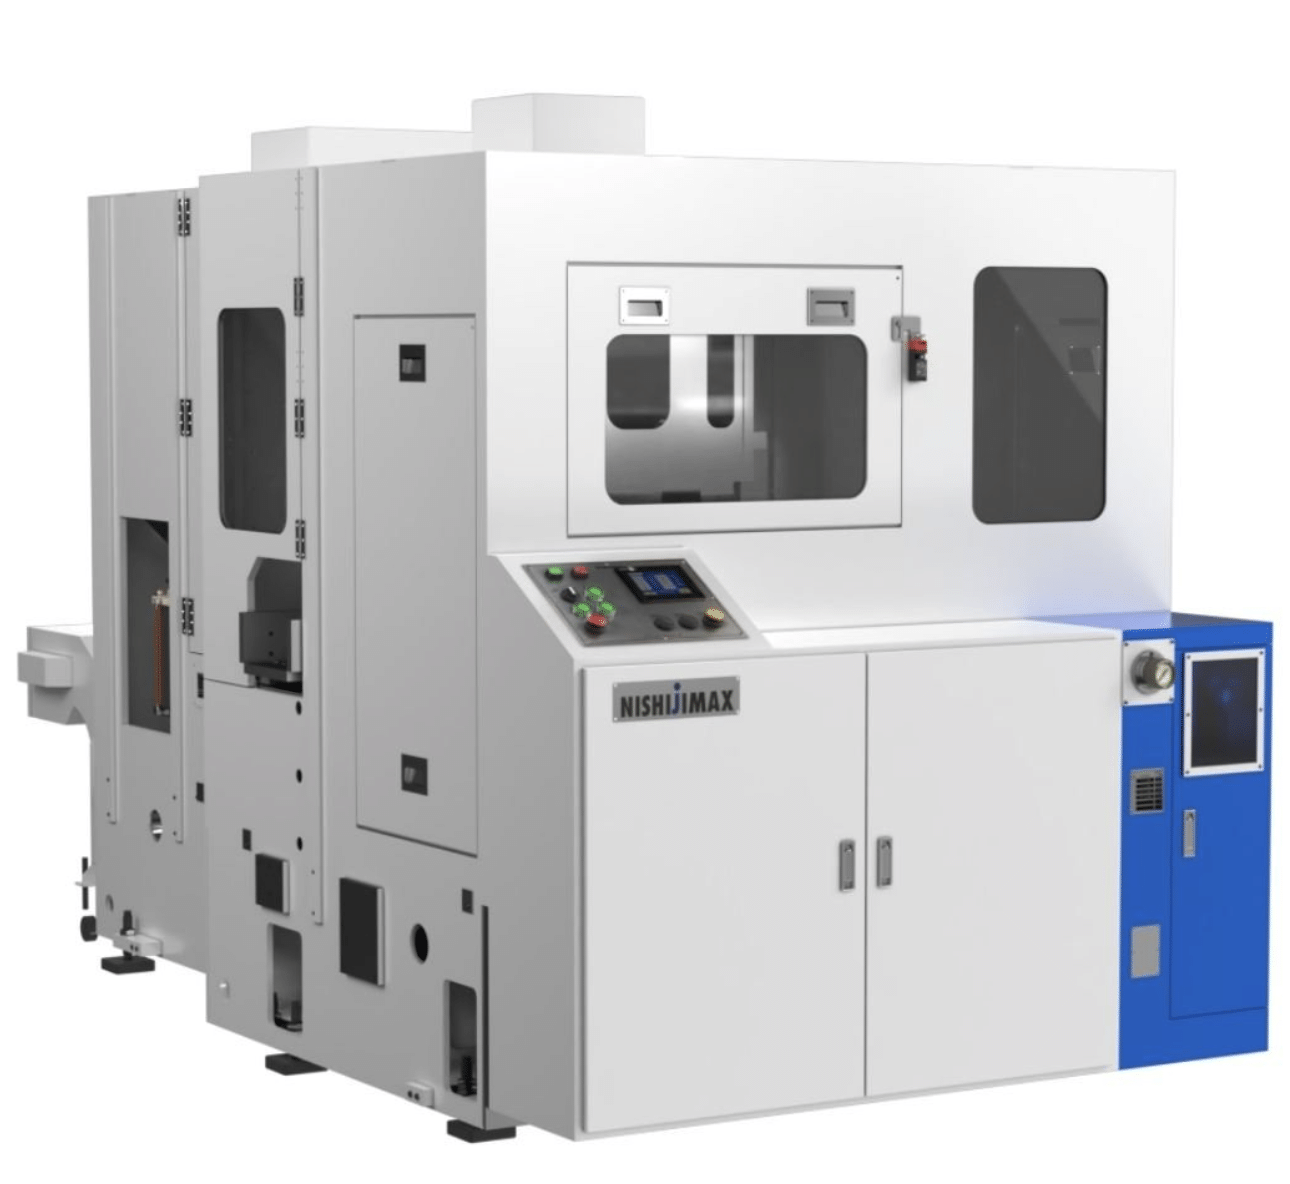
The Pat Mooney NISHIJIMAX NHC-230 is a high-speed circular saw built for demanding production cutting of large-diameter steel bar, tube, and forgings. With capacity for round stock up to 9.06 inches (230 mm), the machine combines a 50 HP saw motor, 29.53-inch circular blade, and servo-controlled cutting and material sizing for consistent, automated cutoff cycles. Its heavy 33,069-pound construction provides a stable platform for manufacturers that need reliable performance when processing substantial ferrous cross sections.
NHC-230 Series (9 inch Cutting Capacity) Features:
The Pat Mooney NHC-230 series combines 9.06-inch round capacity with a 50 HP saw motor and a 29.53-inch blade. That hardware is intended for substantial steel bar, forgings, tube, and pipe where each cut removes considerably more material than the midrange NHC machines.
A 45° slant cutting axis uses AC-servo and ball-screw drive to regulate blade movement, with blade speed adjustable from 20 to 70 RPM. Hydraulic horizontal and vertical clamping stabilizes the work at the cutting and sizing areas, helping control the stock as the blade moves through a large section.
The X-axis provides a 17.72-inch single index for programmed cut lengths. Because the NHC-230 is built around long, heavy material, the saw can be integrated with loading racks, conveyors, and offload equipment so stock movement does not become the bottleneck around the 50 HP cutting process.
| Specification | Value |
| Cutting Capacity | 9.06 in (230 mm) round |
| Cutting Axis | 45° slant cutting axis |
| Saw Motor Power | 50 HP (37 kW) |
| Saw Blade RPM | 20–70 RPM |
| Saw Blade Diameter | 29.53 in (750 mm) |
| Single Index | 17.72 in (450 mm) |
| Machine Weight | 33,069 lb (15,000 kg) |
| Cutting Axis Drive | AC servo motor / ball screw |
| Sizer Axis Drive | AC servo motor / ball screw |
| Clamping | Hydraulic horizontal and vertical |
The Pat Mooney NHC-230 Series is a Nishijimax high-speed carbide circular saw for large bar, pipe, and structural stock. Its configuration places the machine within a defined range of cutoff work rather than treating it as a general-purpose saw.
The 9-inch-capacity platform uses a 45-degree slant saw head, AC-servo and ball-screw cutting feed, a servo-controlled X-axis sizer, close six-point blade guides, horizontal and vertical clamping, and an approximately 33,069-pound machine structure. Final machine selection depends on the complete material range, section geometry, finished length, tolerance, production volume, blade requirements, clamping, material support, and part handling.
Common applications include:
The NHC-230 brings high-speed carbide cutoff production to stock sizes beyond the NHC-180/200 platform.
Independent control of blade speed and saw-head feed allows chip load per tooth to be matched to the stock and material.
Close blade guidance and clamping on both sides of the cut support the workpiece at the blade.
The Mitsubishi PLC and HMI track cutting jobs, blade use, amp load, lubrication status, and machine faults.
The NHC-230 is intended for recurring carbide cutoff production on large bar, pipe, and structural stock requiring capacity through the 9-inch class. Material, section shape, hardness, cut length, and hourly volume define the final process.
The saw head moves on linear rails through an AC-servo motor and ball screw. Blade speed and chip load can be controlled independently, while the X-axis sizer positions the incoming stock for the programmed cut length.
Six-point blade guides, clamping on both sides of the blade, a precision spindle and reduction gearbox, a powered chip brush, micro-drop lubrication, and controlled material retraction all contribute to blade management.
The system can be paired with load tables and bundle racks rated for heavy incoming stock. Bundle holders are available to contain material after steel straps are removed.
Key inputs include stock diameter or section, material grade and hardness, incoming length and bundle weight, finished length and tolerance, parts per shift, remnant target, blade strategy, and exit handling.