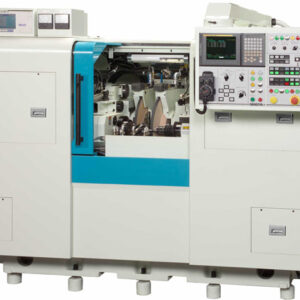
The Shigiya GDP-20-43 is a high-precision production cylindrical grinder built for efficient grinding of shafts and cylindrical components. It delivers consistent accuracy through a rigid machine structure, stable thermal performance, and smooth, repeatable grinding motion during continuous operation. As a result, the GDP-20-43 supports reliable throughput while maintaining tight tolerances and consistent part quality in high-production grinding environments.
The Shigiya GPD-20-43 is a state-of-the-art double-drive CNC cylindrical grinder designed to meet the demanding requirements of modern manufacturing. Its innovative double center drive system eliminates the need for a drive carrier or chuck, allowing for all-step grinding without setup changes. This design significantly reduces setup time and maintenance, enhancing overall productivity. Equipped with NC movable workheads on both the left and right sides, the GPD-20-43 offers adjustable distances between centers, accommodating workpiece lengths ranging from 30mm to 430mm. This flexibility makes it ideal for high-mix mass production lines, where quick adaptation to different workpiece sizes is essential.
The GPD-20-43 utilizes a CBN grinding wheel in conjunction with a multi-step sizing in-process gauge, ensuring consistent processing accuracy and high precision. This combination allows for real-time monitoring and adjustments during the grinding process, maintaining tight tolerances and superior surface finishes. The machine’s swing over table is 200mm, with a maximum grinding diameter of 80mm, and it supports a weight capacity of up to 20kg. These specifications make the GPD-20-43 suitable for a wide range of applications, including automotive, aerospace, and precision engineering industries.
The GPD-20-43’s design focuses on improving processing accuracy and maintenance efficiency. Its double-drive system not only simplifies the setup process but also contributes to improved maintenance by reducing mechanical complexity. This results in increased machine uptime and reduced operational costs. Furthermore, the machine’s compact footprint and robust construction ensure stability during operation, minimizing vibrations and thermal deformation. This stability is crucial for maintaining high-precision grinding over extended periods.
Metric
| Specifications | Units | |
|---|---|---|
| Swing Over Table | mm | 200 |
| Distance Between Centers | mm | 430 |
| Weight Capacity | kg | 20 |
| Machine Weight | kg | 4000 |
| Wheel Size OD | mm | 300 |
| Wheel size width | mm | 30 |
| Wheel spindle | KW | 5.50 |
Standard
| Specifications | Units | |
|---|---|---|
| Swing Over Table | inch | 7.87 |
| Distance Between Centers | inch | 16.93 |
| Weight Capacity | lbs | 44.09 |
| Machine Weight | Ibs | 8818.40 |
| Wheel Size OD | inch | 11.81 |
| Wheel size width | inch | 1.23 |
| Wheel spindle | HP | 4 |
The Shigiya GPD-20-43 is a double-drive CNC cylindrical grinder for all-step grinding without a conventional drive dog or chuck blocking an end of the part. A.W. Miller Technical Sales supplies and supports Shigiya grinding equipment throughout New York, Pennsylvania, Maryland, Delaware, Southern New Jersey, and Quebec, with application engineering, installation, training, and factory-certified service.
The GPD-20-43 provides 200 mm swing, 430 mm between centers, an 80 mm maximum grinding diameter, and a 20 kg between-centers load. NC-movable workheads support part lengths from 30 to 430 mm, and the double-center drive leaves the shaft profile accessible for continuous step grinding. Final machine selection should be based on the complete workpiece, stock allowance, tolerance, surface finish, wheel and dressing package, workholding, gauging, coolant system, automation target, and production rate.
Applications commonly evaluated for the Shigiya GPD-20-43 include:
Driving through both centers eliminates the conventional drive dog or chuck that can block a shaft end, allowing closely spaced diameters and shoulders to be ground in sequence.
Movable workheads accommodate a range of component lengths without rebuilding the complete fixture, supporting mixed-model production when the remaining setup is compatible.
Abrasive type, grade, bond, wheel dimensions, dress form, and dressing interval must be matched to material, stock allowance, finish, and cycle time. The GPD-20-43 process should be validated with the complete wheel and coolant package.
Centers or chucking, drive method, support, coolant filtration, temperature control, and gauge strategy determine whether the GPD-20-43 can hold the required size, roundness, cylindricity, and surface finish through production.
The difference is not limited to nominal swing. Center distance, grinding diameter, supported mass, wheel size, machine footprint, loading method, and available options may change, so both models should be compared against the same representative part family.
It can be configured for precision grinding, but achievable capability depends on part geometry, support, stock, wheel condition, thermal control, setup, and measurement. A process study should define the expected tolerance distribution.
Options may include grinding between centers, chucking, special arbors, center-drive arrangements, steady rests, and dedicated fixtures. Selection follows the part datums, drive torque, accessibility, distortion risk, and finished-surface protection.
In-process gauging is valuable when wheel wear, thermal drift, incoming stock, or long unattended runs could move size outside the required range. Gauge location and compensation logic must be compatible with the feature and cycle.
Provide the full print, material and hardness, starting diameters, stock allowance, grinding lengths, tolerance, finish, wheel specification, dress method, loading time, gauge steps, spark-out, and annual volume.