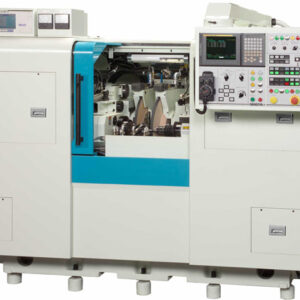
The Shigiya GPES-30 is a versatile cylindrical grinder built for high-precision external grinding across a wide range of part geometries. It delivers stable, repeatable accuracy through a rigid machine structure, smooth axis motion, and consistent thermal performance during extended production cycles. As a result, the GPES-30 supports flexible manufacturing while maintaining tight tolerances and dependable part quality.
The Shigiya GPES-30 stands out as a precision-engineered CNC eccentric grinder built for advanced performance. It is designed to produce highly accurate components, especially those requiring eccentric or irregular shapes. Thanks to its radius traverse function, operators can machine complex profiles efficiently and without secondary operations. This feature adds flexibility to the grinding process, which helps reduce downtime while increasing output. Additionally, the radius traverse system enables more detailed and intricate work. As a result, users can meet strict geometric specifications on a variety of parts.
While it excels at eccentric grinding, the GPES-30 is also a powerful polygon grinding machine. It easily handles the production of shafts and workpieces with non-circular cross-sections. Whether you’re producing splines, couplings, or cam shapes, this machine ensures tight tolerances and smooth finishes. Moreover, its CNC capabilities allow for seamless transitions between profiles. This helps reduce manual intervention and makes production faster and more reliable. With the GPES-30, complex geometries become simple to achieve—without sacrificing quality.
As a high-precision CNC grinder, the GPES-30 delivers excellent accuracy for industries that require consistent part quality. The machine’s rigid frame design and vibration-dampening structure provide stability during prolonged use. Combined with a powerful grinding spindle, the system maintains roundness and finish even under heavy loads. Because of its dependable structure, the GPES-30 excels in both small-batch custom runs and high-volume production. From aerospace components to automotive parts, this grinder performs with excellence.
With a swing over table of 300 mm and center lengths up to 630 mm, the GPES-30 handles various part sizes with ease. Its weight capacity of 66 lbs is ideal for medium-duty applications. Despite its compact footprint, the machine includes robust power through a 15 kW spindle motor, enabling efficient material removal on hardened steels and alloys. Furthermore, the GPES-30’s user-friendly CNC control helps operators quickly switch between part programs. That reduces setup time and increases throughput, especially in busy production environments.
Metric
| Specifications | Units | |
|---|---|---|
| Swing Over Table | mm | 300 |
| Distance Between Centers | mm | 250, 630 |
| Weight Capacity | kg | 30 |
| Machine Weight | kg | 4800 / 6300 |
| Wheel Size OD | mm | 350 |
| Wheel size width | mm | 25 |
| Wheel spindle | KW | 15 |
Standard
| Specifications | Units | |
|---|---|---|
| Swing Over Table | inch | 11.81 |
| Distance Between Centers | inch | 9.84 / 24.81 |
| Weight Capacity | lbs | 66.14 |
| Machine Weight | Ibs | 10582.19 / 13889.12 |
| Wheel Size OD | inch | 13.78 |
| Wheel size width | inch | 0.98 |
| Wheel spindle | HP | 20.12 |
The Shigiya GPES-30 is a specialized CNC cylindrical grinder for production shaft work requiring controlled eccentric, non-round, or feature-specific grinding. A.W. Miller Technical Sales supplies and supports Shigiya grinding equipment throughout New York, Pennsylvania, Maryland, Delaware, Southern New Jersey, and Quebec, with application engineering, installation, training, and factory-certified service.
The GPES-30 is a 30-class specialized platform whose wheelhead, C-axis coordination, workholding, and gauging are selected around the required profile. Maximum swing, center distance, and load should be verified against the exact production specification. Final machine selection should be based on the complete workpiece, stock allowance, tolerance, surface finish, wheel and dressing package, workholding, gauging, coolant system, automation target, and production rate.
Applications commonly evaluated for the Shigiya GPES-30 include:
Axis control and wheel motion are developed around the required non-round or dedicated feature rather than a general cylindrical cycle.
Locating, drive, support, and in-process measurement must be engineered around the exact part family and production tolerance.
Abrasive type, grade, bond, wheel dimensions, dress form, and dressing interval must be matched to material, stock allowance, finish, and cycle time. The GPES-30 process should be validated with the complete wheel and coolant package.
Centers or chucking, drive method, support, coolant filtration, temperature control, and gauge strategy determine whether the GPES-30 can hold the required size, roundness, cylindricity, and surface finish through production.
The GPES-30 is a 30-class specialized platform whose wheelhead, C-axis coordination, workholding, and gauging are selected around the required profile. Maximum swing, center distance, and load should be verified against the exact production specification. The correct size is the smallest configuration that clears the complete part and workholding while meeting load, wheel, and process requirements.
Yes, when the wheel access, program, work support, and gauge plan allow it. Each diameter and shoulder must be checked for collision, stock condition, wheel form, dwell, traverse direction, and dressing demand.
Automation may include loading, chuck or center confirmation, in-process gauging, wheel dressing, part washing, and discharge. A stable manual process should be proven before unattended recovery logic is finalized.
Wheel specification and condition, dress parameters, work speed, traverse or plunge rate, spark-out, coolant delivery, vibration, and incoming stock all affect finish. A slower feed alone does not correct an unstable grinding system.
Flow, pressure, temperature stability, nozzle placement, filtration level, tank capacity, and material contamination must support both the wheel and tolerance. The coolant system should be treated as part of the machine process.