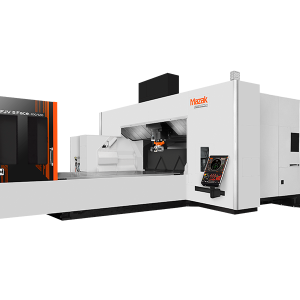

The Mazak Syncrex 12 is a Swiss-type machine engineered for CNC turning on small diameter parts that require high accuracy and process stability. Designed for continuous operation, the Syncrex 12 supports consistent machining performance across demanding production environments where repeatability and tight tolerances are essential. Its robust mechanical design and advanced CNC control make it well suited for manufacturers seeking reliable CNC turning machines for precision component production.
| Model | Syncrex 20/7, Syncrex 20/8, Syncrex 20/9 |
|---|---|
| Max Workpiece Diameter | .472" |
| Max Machining Length | 5.314" |
$1.00
Mazak engineered the Syncrex 12 for production CNC turning on small diameter parts that require dimensional stability and repeatability. Its Swiss-type guide bushing design provides consistent support at the cutting zone, which helps reduce part deflection during machining. As a result, manufacturers can maintain tight tolerances across long production runs while minimizing variation between parts. The Syncrex 12 also supports multiple machining operations in a single setup. This reduces secondary processes and improves overall production efficiency without compromising accuracy.
As one of Mazak’s precision CNC turning machines, the Syncrex 12 is designed to deliver reliable, tight tolerance CNC turning solutions. In addition, the rigid machine structure and precise axis control help maintain stable cutting conditions on complex or slender components. This keeps the surface finish quality and dimensional accuracy consistent throughout extended production cycles. This Mazak Swiss machine also features an integrated CNC control, which enables synchronized motion between machining axes and produces complex parts with minimal operator intervention.
The Mazak Syncrex 12 supports scalable CNC turning solutions for manufacturers operating in high-volume or high-mix production environments. Its compact footprint allows efficient integration into existing shop layouts, while its production-oriented design supports continuous operation with minimal downtime. The Syncrex 12 provides a stable platform for manufacturers seeking to standardize processes, improve throughput, and maintain consistent quality across small-diameter part production.
| Model | Syncrex 20/7, Syncrex 20/8, Syncrex 20/9 |
|---|---|
| Max Workpiece Diameter | .472" |
| Max Machining Length | 5.314" |
| Capacity | Max. machining diameter | Φ12 mm |
|---|---|---|
| Max. machining length GB (one chucking) | 135 mm | |
| Main Spindle | Max. spindle speed | 15000 min-1 |
| Power requirement (40% ED) | 3.7 kW (5 HP) | |
| Second Spindle | Max. spindle speed | 12000 min-1 |
| Power requirement (40% ED) | 3.7 kW (5 HP) | |
| Turret | Number of tools | 24 |
| OD | 7 | |
| Cross live tool | 4 | |
| Back working | 3 | |
| End working tools | 2 | |
| Boring bar holder (Main / Sub) | ||
| Rapid traverse rate | X1-axis | 35000 mm/min |
| Y1-axis | 35000 mm/min | |
| Z1-axis | 35000 mm/min | |
| X2-axis | 35000 mm/min | |
| Y2-axis | 35000 mm/min | |
| Z2-axis | 35000 mm/min | |
| Machine size | Width × Depth (MAZATROL SmoothSt) | 1385 mm × 2242 mm |
| Height | 1050 mm | |
| Weight | 3197 kg |
*B-axis Contouring : 9X Model only
| Capacity | Max. machining diameter | Φ12 mm |
|---|---|---|
| Max. machining length GB (one chucking) | 135 mm | |
| Max. machining length GBL | 30 mm | |
| Main Spindle | Max. spindle speed | 15000 min-1 |
| Power requirement (40% ED) | 3.7 kW (5 HP) | |
| Second Spindle | Max. spindle speed | 12000 min-1 |
| Power requirement (40% ED) | 3.7 kW (5 HP) | |
| Turret | Number of tools | 27 |
| OD | 7 | |
| Cross live tool | 4 | |
| Back working | 6 | |
| End working tools | 2 | |
| Boring bar holder (Main / Sub) | 4 / 4 | |
| Rapid traverse rate | X1-axis | 35000 mm/min |
| Y1-axis | 35000 mm/min | |
| Z1-axis | 35000 mm/min | |
| X2-axis | 35000 mm/min | |
| Y2-axis | 35000 mm/min | |
| Z2-axis | 35000 mm/min | |
| Machine size | Width × Depth (MAZATROL SmoothSt) | 1385 mm × 2242 mm |
| Height | 1770 mm | |
| Weight | 3197 kg |
*B-axis Contouring : 9X Model only
The Mazak Syncrex 12 is a Swiss-type production turning center for miniature shafts, connectors, medical parts, and precision fasteners. Its configuration centers on a 12 mm bar-capacity class, sliding-headstock support, and multi-axis front- and back-working, giving manufacturers a defined platform for parts whose critical features depend on controlled access, stable workholding, and repeatable datum management. A.W. Miller Technical Sales supports machine selection, process development, installation, training, and factory-certified service throughout New York, Pennsylvania, Maryland, Delaware, Southern New Jersey, and Quebec. A.W. Miller Technical Sales is an authorized Mazak distributor serving manufacturers throughout New York, Pennsylvania, Maryland, Delaware, Southern New Jersey, and Quebec, with applications engineering, installation, training, and factory-certified service.
The Syncrex 12 targets very small bar-fed components, using guide-bushing support to control slender stock close to the cut. Machine selection should account for the complete workpiece and fixture envelope, material, spindle load, required tool reach, magazine or turret demand, probing, chip control, and automation plan. Published travels, capacities, spindle ratings, rotary ranges, tool limits, and maximum loads must be checked against the exact machine configuration and part process before purchase.
Parts and processes commonly evaluated for the Mazak Syncrex 12 include:
The capacity is suited to miniature components whose diameter and length demand close stock support.
Main- and sub-spindle operations can finish both ends while reducing manual secondary handling.
Guide-bushing selection, bar straightness, diameter consistency, and remnant strategy directly affect stability on small components. Ground bar stock may be required where tight size control or long length-to-diameter ratios leave little room for variation.
Main-spindle, sub-spindle, and cross-working operations can be divided to keep cutting active and complete the cutoff side. The final sequence must account for tool interference, transfer grip length, chip evacuation, and the most stable location for critical features.
Syncrex 12 is built around a 12 mm bar-capacity class, sliding-headstock support, and multi-axis front- and back-working. That combination can protect feature relationships and remove handling steps when the part is a technical fit.
Features that must remain aligned across different faces or processes benefit most. Examples include bores, diameters, cross holes, angled ports, contours, gear-related geometry, and second-end details as applicable.
No. It can support high-mix or recurring production depending on setup time, tooling, workholding, and automation. The economic case should compare completed-part cycle time and handling, not spindle time alone.
Probing can establish work offsets, verify critical stock, and check selected features in cycle. Final inspection requirements remain tied to the drawing, tolerance stack, and quality plan.
Plan tools by operation, reach, holder clearance, rigidity, life, and magazine demand. Special heads, gear tools, long-reach cutters, or redundant sister tools should be identified before the machine is specified.