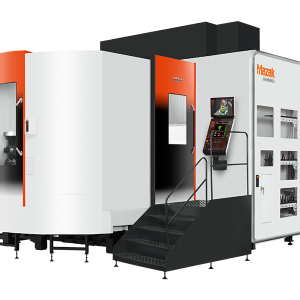
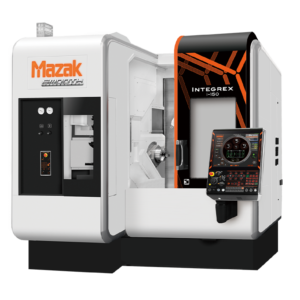
The Mazak HQR 150 is a high-performance multi-tasking CNC machine with automation engineered for fast, precise small-part machining. With dual spindles, dual turrets, and advanced tooling capability, it combines speed, accuracy, and flexibility. Compact in size but powerful in output, it helps manufacturers in medical, electronics, and tooling sectors achieve high-volume throughput without compromising precision.
HQR 15o Features:
| Model | HQR-150MSY |
|---|---|
| Chuck Size | |
| Max Workpiece Diameter | 11.63" |
| Max Machining Length | 24.38" |
The Mazak HQR 150 is a compact yet powerful multi-tasking CNC machine with automation, engineered for speed, precision, and flexibility. For example, it features dual spindles and dual turrets to deliver simultaneous operations. This allows it to cut cycle times, reduce handling, and maintain consistent quality for high-volume or complex work. As a result, it’s ideal for industries such as medical, electronics, and tooling as it balances productivity with accuracy in a compact footprint.
Suitable for small-part production, the HQR 150 combines twin spindles with a dual-turret CNC lathe layout for parallel machining. This setup allows roughing and finishing in one pass, or simultaneous operations on both spindles to improve throughput and consistency. In addition, its rigid construction and symmetrical design ensure stability for high-precision results, even in long production runs.
Engineered as a tooling CNC lathe, the HQR 150 supports live tooling and C-axis control, enabling threading, grooving, milling, and contouring in a single setup. In addition, tool changes are quick and repeatable to reduce downtime. These efficient tool changes also minimize inspections for consistent output and productivity. As a result, it’s ideal for high-mix job shops because of the flexibility ensures precise parts across a wide range of materials and geometries.
Built as a CNC machine with automation, the HQR 150 integrates seamlessly with bar feeders, gantry loaders, and robotic systems. This capability supports lights-out production, reduces labor requirements, and scales with shop growth. With automation driving consistent part flow, manufacturers achieve faster delivery times and higher efficiency without compromising accuracy.
| Model | HQR-150MSY |
|---|---|
| Chuck Size | |
| Max Workpiece Diameter | 11.63" |
| Max Machining Length | 24.38" |
| Universal | Universal type | 600U |
|---|---|---|
| Spindle | Chuck size | 6 “ |
| Max. spindle speed | 5000 rpm | |
| Max. torque (15%ED) | 172 ft-lbs | |
| Spindle motor (30 min. rating) | 15 kW (20 HP) | |
| Spindle motor (cont. rating) | 11 kW (15 HP) | |
| Second spindle | Chuck size | 6 “ |
| Max. spindle speed | 6000 rpm | |
| Spindle motor (30 min. rating) | 11 kW (15 HP) | |
| Spindle motor (cont. rating) | 7.5 kW (10 HP) | |
| Upper and lower turret | Tool storage capacity | 12 |
| Tool shank height | 1 “ | |
| Boring bar shank diameter | Φ1 “ | |
| Rotary tool spindle | Max. spindle speed | 6000 rpm |
| Max. torque (3 min. rating) | 26 ft-lbs | |
| Spindle motor (10 min. rating) | 5.5 kW (7.5 HP) | |
| Spindle motor (cont. rating) | 2.2 kW (3 HP) | |
| Travel | X-axis (upper turret / lower turret) | 7 ” / 4 “ |
| Y-axis (upper turret / lower turret) | 4″ (±2″) / 4″ (±2″) | |
| Z-axis (upper turret / lower turret) | 20 ” / 23 “ | |
| Rapid traverse rate | X-axis (upper turret / lower turret) | 1181 IPM / 945 IPM |
| Y-axis (upper turret / lower turret) | 1024 IPM / 787 IPM | |
| Z-axis (upper turret / lower turret) | 1575 IPM / 1575 IPM | |
| Machine size | Width × Length (MAZATROL SmoothG) | 113 ” × 91 “ |
| Height | 96 “ | |
| Machine weight | 20326 lbs |
The Mazak HQR 150 is a compact dual-spindle, twin-turret turning center for small production parts. Its opposed-spindle arrangement completes the cutoff end while simultaneous turret work supports shorter balanced cycles. A.W. Miller provides regional applications engineering and factory-certified support from the initial process review through installation, training, and production. A.W. Miller Technical Sales is an authorized Mazak distributor serving manufacturers throughout New York, Pennsylvania, Maryland, Delaware, Southern New Jersey, and Quebec, with applications engineering, installation, training, and factory-certified service.
Fixture and tooling plans for the HQR 150 should be developed around 6 in-class chuck capacity with twin spindles, twin turrets, and simultaneous machining capability for small production parts. The final configuration should be checked against the part, fixture, tooling, spindle demand, and automation plan.
Typical process candidates for the Mazak HQR 150 include:
Its compact chuck class targets smaller production components that still require opposed-spindle completion and multi-turret cycle-time reduction.
The part transfers to the opposed spindle so the cutoff end can be faced, turned, drilled, or bored before unloading.
Yes, when the part geometry and program permit coordinated twin-turret cutting without tool or workholding interference.
HQR 150 can be evaluated for production bar work or automated chucking depending on spindle bore, chuck, loading method, and part geometry.
Its compact chuck class targets smaller production components that still require opposed-spindle completion and multi-turret cycle-time reduction.
The part transfers to the opposed spindle so the cutoff end can be faced, turned, drilled, or bored before unloading.
Yes, when the part geometry and program permit coordinated twin-turret cutting without tool or workholding interference.
It can be evaluated for production bar work or automated chucking depending on spindle bore, chuck, loading method, and part geometry.
The balance between spindle-one work, transfer time, spindle-two work, simultaneous cuts, tool changes, and loading establishes the final cycle.